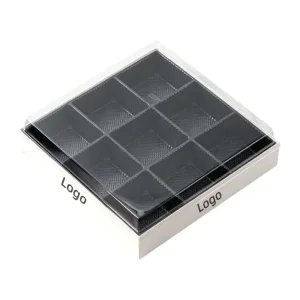
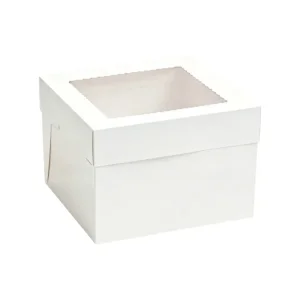
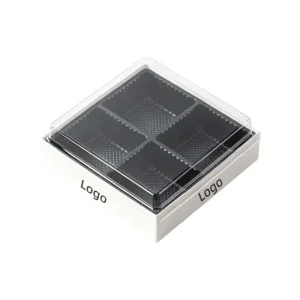
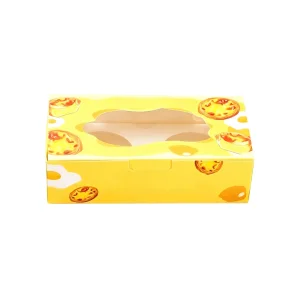
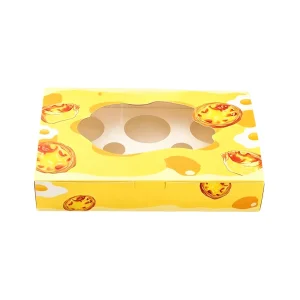
Explore our top-tier OEM/ODM small cardboard and micro-flute box configurations optimized for high structural rigidity, grease isolation, and luxury visual presentation.
In modern global supply chains, small cardboard packaging has evolved from a simple containment vehicle into a precision-engineered brand touchpoint and structural defense mechanism.
Modern small cardboard containers utilize ultra-thin F-flute and N-flute corrugated board (0.6mm–1.0mm) to deliver exceptional crush resistance while drastically cutting down material weight and cubic volume.
With global bans on PFAS and single-use plastics, leading factories rely on bio-based aqueous coatings that yield superior grease, moisture, and oil resistance without compromising recyclability.
Automated high-speed die-cutting and inline folding-glue systems allow factories to hit production rates exceeding 15,000 units per hour while holding strict tolerances of ±0.3mm.
As consumer electronics, gourmet food, cosmetics, and pharmaceuticals demand smaller footprint packaging, manufacturing standards are undergoing rapid technological advancement.
Traditional packaging relied heavily on polyethylene (PE) or polypropylene (PP) film lamination to achieve water and oil repellency. However, plastic-laminated cardboard poses significant challenges in standard repulping operations. The roadmap transitions toward water-based dispersion coatings. These nano-particle aqueous layers create a hydrophobic matrix over virgin fiber while allowing 100% fiber recovery in conventional paper recycling mills.
The demand for sleek, structural boxes has elevated micro-flutes like E-flute (1.5mm), F-flute (0.8mm), and N-flute (0.5mm). By combining double-wall micro-corrugation with calendered linerboards, factories manufacture small boxes that match the smooth print surface of Solid Bleached Sulfate (SBS) while providing 40% higher stacking strength against axial compression.
Future small cardboard packaging integrates conductive inks and micro-thin RFID tags directly into the corrugated fluting. This enables item-level inventory tracking in automated warehouses, cold-chain temperature logging, and interactive consumer unboxing experiences via smartphone scanning without cluttering external box graphics.
Shipping empty pre-assembled boxes creates massive carbon inefficiency. The future belongs to advanced folding structures—such as auto-bottom, crash-lock, and corner-snap configurations—that ship 100% flat and pop open instantly at point-of-use, maximizing container load efficiency without increasing assembly labor costs.
| Substrate Material | Caliper / Weight Range | Structural Rigidity (ECT) | Grease & Moisture Resistance | Sustainability & Recyclability |
|---|---|---|---|---|
| Solid Bleached Sulfate (SBS) | 250 GSM – 400 GSM | Moderate (Bending stiffness) | Low (Requires coating) | 100% Recyclable / Bio-degradable |
| F-Flute Micro-Corrugated | 0.7mm – 1.0mm thickness | High (Superior edge crush) | High (Aqueous dispersion layer) | 100% Recyclable / High yield |
| Recycled Kraft Board (CRB/CCNB) | 300 GSM – 450 GSM | Moderate | Moderate (Sizing agents added) | Made from 85%+ post-consumer fiber |
| Grease-Resistant Coated Board | 280 GSM – 380 GSM | Moderate to High | Extreme (Cobra Test > 1800s) | PFAS-Free / Repulpable certified |
Tailored structural designs matching the rigorous mechanical, thermal, and visual requirements of global market sectors.
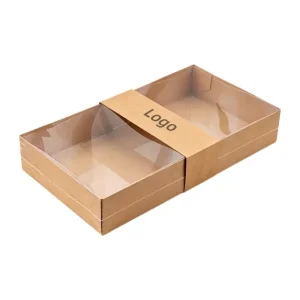
Direct food contact requires strict adherence to FDA 21 CFR 176.170 and EU 1935/2004 standards. Our custom small bakery boxes—such as egg tart boxes, mini cake containers, and pastry carry cartons—feature crystal-clear anti-fog PET windows combined with oil-resistant virgin kraft paperboards, ensuring optical clarity without moisture condensation.
For high-end serums, essential oils, and compact powders, visual tactile sensation drives purchase behavior. We engineer small cardboard boxes featuring soft-touch matte lamination, hot foil stamping (gold/silver/rose gold), tactile embossing, and custom molded pulp or velvet inserts to guarantee zero movement during transit.
Miniaturized tech accessories require anti-static shielding and drop-impact resistance. Using rigid micro-flute board with dense cell structure, our boxes absorb drop shocks from up to 1.5 meters while providing dense printing space for intricate regulatory compliance markings and barcodes.
How advanced automation, localized raw material clusters, and digital quality monitoring empower modern packaging suppliers to outperform legacy manufacturers.
By deploying high-speed Bobst automatic die-cutters and continuous inline folder-gluers equipped with cold/hot adhesive spray monitors, production facilities eliminate manual alignment errors. Photocell inspection systems automatically eject misaligned boxes at full operational speed, ensuring 99.8% zero-defect shipment rates.
Maintaining brand identity across multi-million box runs requires spectral precision. Heidelberg 7-color offset presses outfitted with inline spectrophotometers dynamically adjust ink keys in real-time. This maintains strict color consistency across production batches, limiting variation to a tight Delta E (ΔE) of under 1.2.
Situated in key industrial paper clusters in Guangdong, factories maintain direct raw material pipelines with tier-1 paper mills. Strategic reserves of food-grade virgin kraft, white cardboard, and recycled fluting mitigate global pulp market volatility, ensuring guaranteed pricing stability and rapid order turnaround within 12–15 business days.
Time-to-market is crucial for seasonal products. Utilizing ESKO CAD structural design software and automated digital laser sample cutters, engineering teams transform 3D CAD files into physical, functional pre-production prototypes within 24 to 48 hours for immediate physical testing.
International brands and enterprise packaging buyers require robust documentation, environmental certifications, and audited quality management protocols.
All small cardboard boxes engineered for direct food contact undergo third-party SGS/Intertek laboratory testing. Certification reports verify compliance with FDA 21 CFR 176.170, EU 1935/2004, and German LFGB recommendations, proving zero migration of heavy metals, mineral oils (MOSH/MOAH), or fluorinated chemicals.
To support corporate ESG goals, paperboard substrates are sourced from FSC-certified (Forest Stewardship Council) managed forests. Full Chain-of-Custody (CoC) documentation ensures that every fiber trace can be tracked back to ethically managed, renewable forestry operations.
Manufacturing facilities maintain active ISO 9001:2015 Quality Management and BRCGS (British Retail Consortium Global Standard) Packaging Materials certifications, ensuring smooth factory audits for major global importers and multinational supermarket chains.
Key technical and commercial inquiries answered by our senior packaging engineering team.
Explore our complete range of specialized bakery boxes, cake bases, catering trays, and multi-compartment containers.