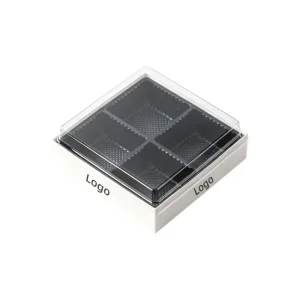
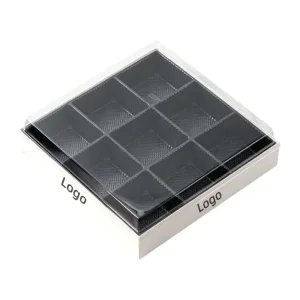
Direct factory engineering solutions optimized for shelf visual impact, structural integrity, and sustainable food-grade barrier performance.
In the global confectionery sector, packaging is no longer merely a passive transport vessel; it functions as a critical engineering barrier and the primary vehicle for brand equity monetization. The global premium chocolate market—projected to surpass USD 38.5 Billion by 2030—is experiencing a radical shift toward eco-engineered cardboard substrates. Driven by aggressive environmental regulations across the European Union (such as the Packaging and Packaging Waste Regulation - PPWR) and evolving consumer demands in North America and Asia-Pacific, brand owners are systematically replacing expanded polystyrene (EPS) and non-recyclable single-use plastics with advanced virgin fiberboard, rigid box set-ups, and biodegradable barrier-coated paperboard.
As a premier direct OEM/ODM manufacturer operating within China's primary packaging industrial cluster in Chaozhou, Guangdong, our manufacturing infrastructure bridges the gap between complex biochemical preservation requirements and commercial cost efficiency. High-end chocolates—specifically single-origin dark chocolate, artisan pralines, and ganache-filled bonbons—are susceptible to environmental degradation caused by relative humidity, oxygen exposure, fat bloom migration, and odor cross-contamination.
Achieving commercial success requires selecting a certified manufacturing partner capable of executing strict industrial tolerances. From managing precise Water Vapor Transmission Rates (WVTR) to engineering magnetic closure mechanisms that maintain tactile luxury, our factory provides enterprise buyers with complete technical execution from die-line structural CAD creation to high-volume automated box assembly.
China’s packaging industrial ecosystem—particularly the Chaozhou packaging cluster—offers unprecedented structural advantages for overseas procurement directors, wholesale distributors, and retail chain buyers. By integrating paper mills, die-tooling foundries, high-speed offset printing presses, and automated rigid box assembly lines within a tight geographic radius, our facility eliminates supply chain friction and provides significant unit-cost efficiency.
Utilizing state-of-the-art German and Japanese automatic box-making machinery (including Heidelberg offset presses and Hongming automatic rigid box formers), we achieve precise registration tolerances within ±0.2mm, ensuring flawless corners, seamless V-cut grooving, and crisp edge alignment.
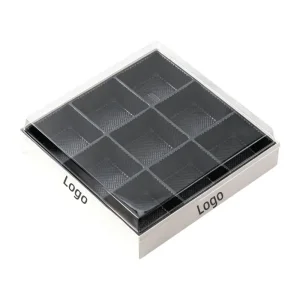
With over 1,500 standard die-cuts and thermoforming blister moulds already engineered, we eliminate NRE (Non-Recurring Engineering) tooling costs for clients selecting standard grid configurations (e.g., 4, 6, 9, 12, 16, and 24-piece chocolate trays).
Rigid gift boxes traditionally suffer from excessive ocean freight costs due to high volumetric weight. Our structural R&D team has pioneered collapsible rigid box structures with pre-applied 3M adhesive strips, reducing container volume by up to 35% during transit.
Selecting the correct paperboard substrate is vital to preventing fat migration (which stains untreated paperboard) and maintaining structural rigidity under high-stacking warehouse environments. Below is our comprehensive engineering matrix for custom chocolate cardboard packaging:
| Substrate Material | Grammage / Thickness Range | Primary Barrier Coating | Food Compliance Standard | Recommended Packaging Application |
|---|---|---|---|---|
| Virgin Solid Bleached Sulfate (SBS) | 250 gsm – 450 gsm | Water-based Dispersion / PE Lamination | FDA 21 CFR 176.170 / LFGB Section 31 | High-definition offset printed folding cartons, sleeves, and tuck boxes. |
| Unbleached Kraft Board | 230 gsm – 400 gsm | Bio-Wax / Grease-Proof Coating (KIT 8-12) | EU Regulation (EC) No 1935/2004 | Artisan organic chocolate bars, eco-friendly rustic retail packaging. |
| Greyboard (Rigid Box Core) | 1.2 mm – 3.0 mm (800–1800 gsm) | Wrapped with 157 gsm Art Paper / Specialty Paper | RoHS / Heavy Metal Free Certified | Luxury set-up boxes, rigid shoulder boxes, magnetic closure presentation cases. |
| Food-Grade Food PET Lids / Trays | 0.25 mm – 0.50 mm sheet thickness | Anti-static / High-Clarity Anti-Fog Coating | REACH / Direct Food Contact Grade | Internal compartment grid dividers, thermoformed protective trays, clear windows. |
| E/F Flute Corrugated Board | 1.5 mm – 2.0 mm wall thickness | Varnish / Matte Lamination | GB 4806.8-2016 Food Contact Standard | Heavy-duty ecommerce mailer chocolate boxes, bulk wholesale delivery trays. |
Different global markets require specialized packaging configurations to meet local consumer preferences, logistics constraints, and retail display standards. Our OEM manufacturing facility tailors designs specifically for four dominant commercial scenarios:
Market Dynamics: High SKU variation, short seasonal runs (Valentine's Day, Easter, Christmas), requirement for low minimum order quantities (MOQs).
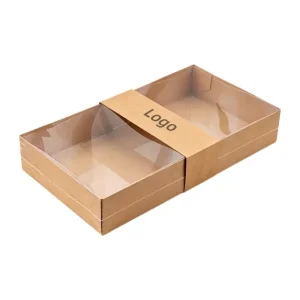
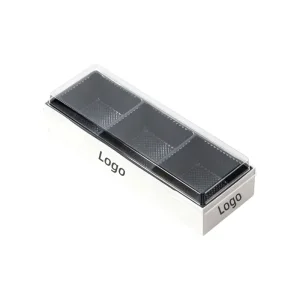
Engineered Solution: Modular base rigid boxes paired with customizable foil-stamped outer sleeves. Standardized 9-grid and 16-grid food-grade PET trays allow confectioners to keep single box sizes while updating seasonal artwork effortlessly.
Market Dynamics: High-speed automated packing lines, extreme price sensitivity per unit, strict drop-test and stacking strength requirements.
Engineered Solution: Auto-bottom tuck end SBS paperboard cartons with integrated high-clarity PET windows. Designed for auto-assembly machines with high structural compression ratings to eliminate box collapse on supermarket shelves.
Market Dynamics: Unboxing experience driving premium margins, requirement for security tamper-evident seals and heavy tactile feel.
Engineered Solution: Heavyweight 2.5mm greyboard rigid book-style boxes, featuring soft-touch velvet lamination, metallic hot-foil stamping, debossed logos, and concealed neodymium magnetic clasps.
As environmental sustainability transitions from a marketing preference to a legal imperative globally, packaging engineers are forced to innovate beyond conventional plastic-laminated boards. Our factory R&D center is actively pioneering three key technological advances:
Replacing traditional polyethylene (PE) and polypropylene (OPP) plastic films with water-based dispersion barriers. This allows the finished chocolate box to be repulped in standard municipal paper recycling streams without requiring chemical separation.
Designing entire rigid gift box assemblies—including internal tray inserts—from 100% paper pulp or molded sugarcane bagasse, achieving complete circularity for eco-conscious luxury brands.
Embedding invisible UV fluorescent inks, unique micro-QR codes, and NFC tags into the packaging matrix during printing, allowing premium chocolatiers to verify product authenticity and engage consumers directly via smartphone scans.
Direct engineering answers addressing critical procurement, compliance, and structural parameters for enterprise sourcing managers.
Comprehensive packaging solutions ranging from clear treat bags to specialized festive gift packaging.